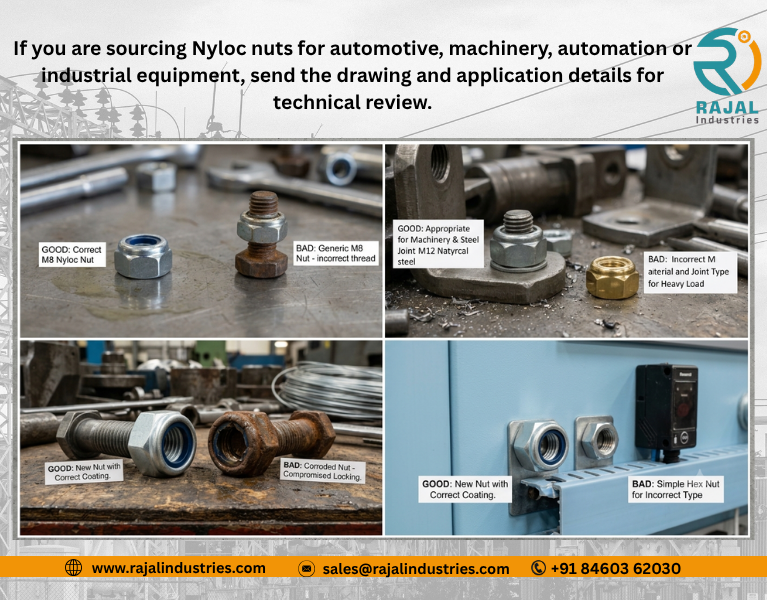
Selecting the correct Nyloc Nut Sizes requires more than choosing an M6, M8, M10 or M12 thread.
A Nyloc-type nut is a prevailing-torque fastener. Its non-metallic insert interacts with the mating bolt thread and creates rotational resistance.
Industrial buyers should therefore select it using:
Thread → Pitch → Nut Type → Standard → Dimensions → Mechanical Requirement → Material → Insert → Coating → Mating Bolt → Temperature → Prevailing Torque
This is especially important for automotive, machinery, automation and industrial equipment where consistent assembly and locking performance matter.
What Are Nyloc Nut Sizes?
Nyloc Nut Sizes are defined by the internal thread plus the dimensions and product form of the prevailing-torque nut. Important factors include thread diameter, pitch, width across flats, nut-body height, overall height including the locking feature, material, mechanical properties and applicable standard.
An M8 Nyloc nut is therefore not completely specified by the word:
M8
What Does M8 Nyloc Nut Mean?
An M8 Nyloc nut has a nominal metric internal thread diameter of:
8 mm
For a common coarse thread:
M8 × 1.25
But that still does not define:
- Regular, high or thin nut
- Overall height
- Width across flats
- Mechanical requirement
- Material
- Coating
- Insert
- Functional prevailing torque
The applicable standard or customer drawing is still required.
Common Metric Nyloc Nut Thread Sizes
Depending on the applicable standard, metric non-metallic-insert prevailing-torque nuts cover a broad range.
Common OEM requirements include:
| Thread | Common Coarse Pitch |
| M3 | 0.5 mm |
| M4 | 0.7 mm |
| M5 | 0.8 mm |
| M6 | 1.0 mm |
| M8 | 1.25 mm |
| M10 | 1.5 mm |
| M12 | 1.75 mm |
| M14 | 2.0 mm |
| M16 | 2.0 mm |
| M20 | 2.5 mm |
| M24 | 3.0 mm |
Larger sizes can also fall within applicable ISO product ranges.
The actual product standard should control.
M3 Nyloc Nut
M3 is used in suitable smaller assemblies such as:
- Electronics equipment
- Light automation
- Instruments
- Small brackets
- Equipment covers
The designer should still check:
- Nut type
- Available space
- Mating screw
- Mechanical requirement
- Insert performance
Small size does not remove the need for correct joint design.
M4 Nyloc Nut
M4 can suit suitable:
- Electrical equipment
- Automation components
- Light machinery
- Instrumentation
- Enclosures
For automated assembly, thread start and prevailing-torque consistency can be particularly important.
M5 Nyloc Nut
M5 is common in suitable:
- Equipment
- Machinery guards
- Automotive components
- Automation
- Electrical assemblies
ISO 2320’s functional scope for coarse-thread prevailing-torque steel nuts starts at M5.
This does not mean smaller ISO product-standard nuts do not exist. For example, ISO 7040:2025 covers regular products down to M3.
M6 Nyloc Nut
M6 is widely encountered in:
- Machinery
- Automation equipment
- Brackets
- Equipment frames
- Automotive assemblies
Selection should still include:
M6 × Pitch + Nut Type + Standard + Mechanical Requirement + Finish
Do not purchase only by diameter.
M8 Nyloc Nut
M8 is frequently used in industrial equipment and machinery.
Important checks include:
- M8 × 1.25 coarse or specified fine pitch
- Regular/high/thin type
- Mechanical compatibility with bolt
- Coating
- Temperature
- Prevailing torque
M10 Nyloc Nut
M10 can be used in suitable:
- Machinery
- Industrial equipment
- Automotive assemblies
- Material-handling equipment
Do not assume a larger nut automatically provides better vibration performance.
The complete joint determines performance.
M12 Nyloc Nut
M12 requirements may vary significantly depending on:
- Thread pitch
- Nut type
- Bolt properties
- Service load
- Temperature
- Coating
A complete RFQ should identify all of these.
M14 and M16 Nyloc Nuts
Larger locking nuts can be used in suitable equipment and machinery.
As size and joint load increase, mechanical compatibility with the mating bolt becomes increasingly important.
Do not specify a generic:
for an engineered joint without additional requirements.
Nyloc Nut Size Does Not Define Strength
This distinction is critical.
For example:
M10
defines the nominal thread diameter.
It does not independently define:
- Nut property requirement
- Nut material
- Heat treatment
- Proof capability
- Coating
- Prevailing torque
Size and mechanical properties are separate specification elements.
Main Nyloc Nut Dimensions
Important Nyloc Nut Dimensions can include:
d — Thread Diameter
The nominal internal thread diameter.
P — Thread Pitch
The distance between adjacent metric thread forms.
s — Width Across Flats
The hexagonal wrenching dimension.
m — Nut-Body Height
The relevant metal nut-body dimension under the applicable product design.
h — Overall Height
The total product height including the prevailing-torque feature.
Exact symbols and definitions should follow the applicable standard or drawing.
Why Overall Height Matters
A Nyloc nut contains an additional prevailing-torque feature above the basic nut body.
Therefore, overall height matters for:
- Assembly clearance
- Bolt length
- Tool access
- Nearby components
- Packaging of the joint
This is particularly important in compact machinery and automation systems.
Width Across Flats
Width across flats affects:
- Socket selection
- Wrench access
- Automated tool access
- Assembly envelope
Do not assume all lock nuts with the same thread have the same external dimensions.
The applicable product standard controls.
Regular vs High vs Thin Nyloc Nut Dimensions
Current ISO standards distinguish three important coarse-thread product forms:
| Product Form | Current ISO | Coarse Thread Range |
| Regular | ISO 7040:2025 | M3–M39 |
| High | ISO 7041:2025 | M5–M39 |
| Thin | ISO 10511:2025 | M3–M39 |
All three cover steel and stainless-steel products with product grades A and B within their respective scopes.
ISO 7040:2025 Regular Nyloc Nut
ISO 7040:2025 specifies regular prevailing-torque hexagon nuts with non-metallic inserts.
Its scope covers:
- Steel
- Stainless steel
- Metric coarse pitch
- M3 to M39
- Product grades A and B
ISO states that the regular nut’s overall height is based on the relevant style-1 minimum nut height plus the prevailing-torque feature.
ISO 7041:2025 High Nyloc Nut
ISO 7041:2025 covers high prevailing-torque hexagon nuts with non-metallic inserts.
Its scope includes:
- Steel
- Stainless steel
- Metric coarse pitch
- M5 to M39
- Product grades A and B
The high design uses the relevant style-2 nut-height basis plus the prevailing-torque feature.
ISO 10511:2025 Thin Nyloc Nut
ISO 10511:2025 covers thin prevailing-torque hexagon nuts with non-metallic inserts.
Its scope includes:
- Steel
- Stainless steel
- Metric coarse pitch
- M3 to M39
- Product grades A and B
Its geometry uses the relevant style-0 nut-height basis plus the prevailing-torque feature.
Interesting ISO Design Detail
The current ISO product standards state that, for a given nominal diameter, the height of the non-metallic prevailing-torque feature is identical across the regular, high and thin families.
The difference in overall height comes from the underlying nut-body style.
This is useful for buyers comparing product families.
Regular vs High vs Thin Selection
| Requirement | Regular | High | Thin |
| General OEM Use | Common option | Application-specific | Application-specific |
| Overall Height | Medium | Greater | Lower |
| Space Requirement | Normal | Greater | Reduced |
| Nut Body Style | Style 1 basis | Style 2 basis | Style 0 basis |
| Coarse ISO Family | ISO 7040 | ISO 7041 | ISO 10511 |
| Selection | Joint-specific | Joint-specific | Joint-specific |
Do not substitute between these families only because the thread matches.
Thin Nyloc Nut Selection Requires Extra Care
A thin nut provides reduced body height.
That can be useful when:
- Axial space is limited
- Equipment is compact
- The drawing specifically requires a thin design
But reduced height changes the mechanical behaviour and available thread engagement.
Do not use a thin nut simply to reduce cost or save space without engineering review.
Fine-Pitch Nyloc Nut Sizes
Not every Nyloc nut uses a coarse metric thread.
ISO 10512:2025 covers:
Prevailing torque hexagon regular nuts with non-metallic insert, with fine pitch thread.
Its scope includes metric fine-pitch threads from nominal diameter 8 mm to 39 mm, in steel and stainless steel, with product grades A and B.
Fine-Pitch Thread Example
A buyer may encounter:
M12 × 1.75 — common coarse pitch
and:
M12 × 1.5 — fine pitch example
These are not interchangeable.
Both the nut and bolt must have the same approved thread.
Fine Thread Is Not Automatically Better
Fine-pitch threads can be useful for certain engineered joints, but do not claim that they are universally:
- Stronger
- More vibration resistant
- More precise
- Better for automotive
The application and joint design should determine thread pitch.
Current ISO Standards for Nyloc-Type Nuts
| Standard | Product | Thread |
| ISO 7040:2025 | Regular non-metallic-insert prevailing-torque nut | Coarse |
| ISO 7041:2025 | High non-metallic-insert prevailing-torque nut | Coarse |
| ISO 10511:2025 | Thin non-metallic-insert prevailing-torque nut | Coarse |
| ISO 10512:2025 | Regular non-metallic-insert prevailing-torque nut | Fine |
| ISO 2320:2015 | Functional properties for prevailing-torque steel nuts | Coarse + fine within scope |
ISO 2320:2015 was reviewed and confirmed in 2025, so it remains current.
Product Standard vs Functional Standard
This is important for OEM procurement.
Product Standard
Defines the characteristics of the particular nut family.
Examples:
- ISO 7040
- ISO 7041
- ISO 10511
- ISO 10512
Functional Standard
ISO 2320 addresses functional properties of prevailing-torque steel nuts within its defined scope.
A nut can look dimensionally correct but still require functional verification.
What Does ISO 2320 Cover?
ISO 2320:2015 covers functional properties for prevailing-torque steel nuts under its specified test conditions.
Its scope includes:
- All-metal prevailing-torque nuts
- Non-metallic-insert prevailing-torque nuts
- Coarse threads M5–M39
- Fine threads M8 × 1 to M39 × 3
within its other specified thread and mechanical-property conditions.
Important M3 and M4 Distinction
ISO 7040:2025 and ISO 10511:2025 include product designs down to M3.
However, ISO 2320’s stated coarse-thread functional scope begins at M5.
Therefore, buyers should not automatically apply ISO 2320 M5–M39 functional criteria to M3 or M4 products.
This is exactly why the product standard and functional standard should be checked separately.
Product Grade A and B
The current ISO 7040, 7041, 10511 and 10512 product standards specify product grades A and B within their scopes.
Product grade relates to dimensional/product requirements.
It should not be confused with:
- Property class
- Material grade
- Stainless grade
- Insert grade
Product Grade vs Property Class
Product Grade
Deals with product/dimensional accuracy requirements.
Property Class
Deals with specified mechanical properties.
They are not the same.
An RFQ should not state only:
Grade A Nyloc nut
when the buyer actually means a mechanical property class.
Nyloc Nut Materials
The current ISO product families discussed above include both:
- Steel
- Stainless steel
within their specified scopes.
The correct material should follow:
Mechanical Requirement + Corrosion + Temperature + Mating Bolt + OEM Specification
Steel Nyloc Nuts
Steel Nyloc nuts can suit many:
- Automotive
- Machinery
- Equipment
- Automation
applications.
The buyer should additionally define:
- Mechanical/property requirement
- Coating
- Corrosion requirement
- Functional requirement
Stainless Steel Nyloc Nuts
Stainless can be selected for suitable corrosion-resistant applications.
Important considerations include:
- Stainless grade/property requirement
- Mating bolt
- Galling
- Environment
- Insert limitations
- Cost
Do not assume:
Stainless = A4/316.
Stainless Mechanical Properties
The current ISO product standards note that, where applicable, stainless grades can be selected from ISO 3506-2.
The actual grade must still be specified according to the application.
Steel Nut Mechanical Properties
Current product-standard notes reference ISO 898-2 for applicable steel-nut property classes where other specifications are requested.
Do not assign a mechanical property class solely from nut size.
Nyloc Nut Insert
The non-metallic insert is the defining functional feature.
Its purpose is to interact with the bolt thread and create prevailing torque.
Important insert characteristics can include:
- Material
- Geometry
- Position
- Retention
- Temperature behaviour
- Chemical compatibility
Is the Insert Always Nylon?
“Nyloc” and “nylon insert lock nut” are widely used commercial terms.
However, technical ISO terminology is:
Non-metallic insert
That terminology is safer for standards-based specification because the exact insert material can be product/manufacturer-specific.
Insert Colour
Insert colours can include various shades depending on supplier and product.
Do not use colour as a universal indicator of:
- Material
- Temperature rating
- Property class
- Prevailing torque
- Quality level
Use the technical specification.
Insert Height and Overall Nut Height
Current ISO standards distinguish:
Basic Nut-Body Height + Prevailing-Torque Feature Height = Overall Product Height
This explains why a Nyloc-type nut is taller than the underlying basic nut-body geometry.
Exact dimensions should come from the controlled standard or drawing.
Nyloc Nut Dimensions and Tool Access
Before selecting the nut, check:
- Socket size
- Wrench access
- Nut height
- Nearby components
- Bolt protrusion
- Installation tool
This matters in compact automation and machinery.
Automated Assembly Clearance
An automatic nut runner may require more space than a hand wrench.
Therefore:
Nut Dimensions + Socket Dimensions + Tool Clearance
should be reviewed during equipment design.
Bolt Length Selection
Bolt length should provide sufficient engagement through the nut and locking feature according to the approved joint design.
Too short can create inadequate engagement.
Too long can cause:
- Interference
- Excess projection
- Safety/packaging problems
Do not use a universal exposed-thread rule for every assembly.
Mating Bolt Compatibility
Always check:
Nut Thread ↔ Bolt Thread
and:
Nut Mechanical Requirement ↔ Bolt Mechanical Requirement
plus:
Nut Coating ↔ Bolt Coating
The locking feature interacts directly with the bolt thread.
Bolt Thread Quality Matters
A damaged or uncontrolled bolt can change:
- Prevailing torque
- Installation torque
- Insert wear
- Removal behaviour
For functional qualification, use an approved or controlled mating fastener.
Nyloc Nut Surface Finishes
Possible steel-nut coating systems can include suitable:
- Zinc electroplating
- Zinc-flake coatings
- Other customer-specified finishes
Selection should consider:
- Corrosion
- Friction
- Thread fit
- OEM requirement
- Prevailing-torque behaviour
Coating Changes Assembly Behaviour
Coating can influence:
- Thread friction
- Bearing friction
- Thread dimensions
- Surface interaction
Therefore:
Changing coating can change tightening behaviour.
Do not transfer a validated tightening process blindly from one coating system to another.
Coating and Prevailing Torque
The locking feature interacts with the coated or finished bolt thread.
Therefore, bolt coating can also influence measured prevailing torque.
Functional validation should represent production conditions where required.
Nyloc Nut Temperature
Temperature is a major selection factor because the locking feature contains a non-metallic insert.
ISO 2320 states that non-metallic-insert nuts conforming to its requirements are used in applications ranging from −50 °C to +120 °C, while also warning that temperature influences functional properties.
This should not be converted into a universal temperature rating for every commercial Nyloc nut.
Why the Temperature Range Needs Context
ISO 2320’s functional tests themselves are specified at an ambient range of +10 °C to +35 °C.
Actual suitability still depends on:
- Product
- Insert material
- Service exposure
- Thermal cycling
- Chemicals
- OEM requirements
High-Temperature Applications
For temperatures outside the validated capability of the non-metallic insert, an all-metal prevailing-torque nut may need evaluation.
Do not automatically specify Nyloc nuts near:
- Exhaust systems
- Furnaces
- High-temperature process equipment
without reviewing the actual thermal environment.
Chemical Exposure
A Nyloc nut used in industrial equipment may contact:
- Oil
- Coolant
- Fuel
- Cleaning agents
- Hydraulic fluids
- Process chemicals
Compatibility should be checked against the actual insert material.
Prevailing Torque
Prevailing torque is rotational resistance created by the locking feature.
It is not the same as:
- Tightening torque
- Clamp load
- Proof load
- Joint strength
This distinction is essential for engineering selection.
ISO 2320 Laboratory Conditions
ISO 2320 explicitly notes that its specified prevailing-torque values are based on laboratory test conditions and that actual prevailing torque in practical applications can vary.
Therefore, do not treat one catalogue value as a guaranteed production-assembly torque.
Nyloc Nut Tightening
A Nyloc nut still requires the correct joint tightening process.
Conceptually, the installation tool experiences effects from:
Prevailing Torque + Thread Friction + Bearing Friction + Clamp-Load Generation
The actual relationship depends on the joint.
No Universal Torque Chart
Do not publish generic statements such as:
M8 Nyloc Nut = X Nm
without defining:
- Bolt property
- Nut property
- Coating
- Lubrication
- Friction
- Joint
- Required preload
Torque should follow the approved engineering specification.
Nyloc Nut Reuse
Repeated installation can change the locking feature’s behaviour.
Therefore:
Reuse should not be assumed.
The OEM or maintenance specification should define whether reuse is allowed and what functional acceptance criteria apply.
No Universal Reuse Count
Avoid statements such as:
Nyloc nuts can be reused five times.
There is no universal count that applies to every product and application.
Nyloc Nut Size Selection by Industry
Automotive
Check:
Thread + Standard + Mechanical Properties + Coating + Temperature + Prevailing Torque + PPAP
Machinery
Check:
Load + Vibration + Bolt + Temperature + Oil/Coolant + Maintenance
Equipment
Check:
Joint + Corrosion + Service Access + Locking Requirement
Automation
Check:
Thread + Prevailing-Torque Consistency + Tool Access + Cycle Time + Tightening Strategy
Automotive Nyloc Nut Sizes
Automotive applications may use different sizes depending on the component.
Do not create a rule such as:
M6 = automotive interior
M10 = chassis
Vehicle design and OEM specifications vary.
Use the actual drawing.
Machinery Nyloc Nut Sizes
Machinery applications should select the thread from the joint load and bolt requirement first.
Then choose the appropriate locking-nut family.
Do not increase nut size merely because the machine vibrates.
Automation Nyloc Nut Sizes
Automation systems may place additional importance on:
- Tool access
- Run-down behaviour
- Prevailing-torque consistency
- Cross-thread detection
- Cycle time
A technically acceptable nut can still create production problems if functional variation is excessive.
Nyloc Nut vs All-Metal Lock Nut
| Factor | Non-Metallic Insert | All-Metal |
| Locking Feature | Non-metallic insert | Metallic deformation/geometry |
| Temperature | Insert must be evaluated | Often considered for higher-temperature use |
| Chemical Compatibility | Insert important | Different considerations |
| Prevailing Torque | Product-specific | Product-specific |
| Reuse | Validate | Validate |
| Selection | Application-specific | Application-specific |
Neither is universally better.
Nyloc Nut vs Standard Hex Nut
A standard hex nut normally does not contain a prevailing-torque feature.
If an OEM changes from a standard nut to a Nyloc-type nut, review:
- Tightening
- Bolt length
- Clearance
- Temperature
- Tooling
- Reuse
- Cost
Do not treat it as a simple drop-in change.
Common Nyloc Nut Selection Mistakes
Avoid:
- Ordering only by M-size.
- Ignoring thread pitch.
- Mixing regular, high and thin designs.
- Assuming all insert colours mean the same thing.
- Ignoring bolt mechanical properties.
- Ignoring bolt coating.
- Using generic torque charts.
- Assuming unlimited reuse.
- Calling the nut vibration proof.
- Ignoring temperature.
- Ignoring chemical exposure.
- Approving only by dimensions.
- Assuming stainless means 316.
- Using ISO 2320 criteria outside its scope without review.
Nyloc Nut Selection Workflow
Use:
Step 1
Define the application.
Step 2
Identify the mating bolt.
Step 3
Select thread diameter.
Step 4
Select pitch.
Step 5
Choose regular/high/thin design.
Step 6
Identify product standard.
Step 7
Specify nut mechanical properties.
Step 8
Select material.
Step 9
Define insert requirement where necessary.
Step 10
Select coating.
Step 11
Check temperature and chemicals.
Step 12
Define prevailing-torque requirements.
Step 13
Define tightening process.
Step 14
Validate samples in the real assembly.
Nyloc Nut RFQ Checklist
Provide:
☐ Product standard
☐ Standard edition where controlled
☐ Thread diameter
☐ Thread pitch
☐ Regular/high/thin type
☐ Nut dimensions if custom
☐ Material
☐ Mechanical/property requirement
☐ Insert specification if required
☐ Coating
☐ Mating bolt
☐ Bolt coating
☐ Service temperature
☐ Chemical exposure
☐ Prevailing-torque requirement
☐ Tightening requirement
☐ Reuse policy
☐ Testing
☐ PPAP/documentation
☐ Quantity
☐ Annual demand
Example: Automotive RFQ
Product: Nylon Insert Lock Nut
Thread: M8 × 1.25
Product Type: Regular
Standard: Applicable ISO/customer drawing
Mechanical Requirement: Customer specification
Coating: OEM specification
Mating Bolt: Drawing attached
Prevailing Torque: Customer functional requirement
Temperature: Application data attached
PPAP: Required
Annual Quantity: 1,000,000 pcs
Example: Machinery RFQ
Product: Nyloc Lock Nut
Thread: M10 × 1.5
Nut Type: Regular non-metallic-insert prevailing-torque nut
Material/Mechanical Requirement: Drawing attached
Finish: Specification attached
Mating Bolt: Attached
Environment: Industrial machinery with oil exposure
Testing: Prevailing-torque testing required
Quantity: 250,000 pcs/year
What Are Common Nyloc Nut Sizes?
Common Nyloc Nut Sizes include M3, M4, M5, M6, M8, M10, M12, M14 and M16, with larger sizes available under applicable product standards. The correct nut must also be selected by pitch, product type, mechanical properties and standard.
What Standard Covers Nyloc Nut Sizes?
Current standards include ISO 7040:2025 for regular coarse-thread non-metallic-insert nuts, ISO 7041:2025 for high coarse-thread nuts, ISO 10511:2025 for thin coarse-thread nuts and ISO 10512:2025 for regular fine-pitch nuts.
What Is the Difference Between Regular and Thin Nyloc Nuts?
A regular Nyloc nut uses a standard style-1 nut-body basis, while a thin Nyloc nut uses a reduced style-0 nut-body basis. This changes overall height and mechanical behaviour, so they should not be substituted only because the thread matches.
Are Fine-Pitch Nyloc Nuts Available?
Yes. ISO 10512:2025 covers regular non-metallic-insert prevailing-torque nuts with metric fine-pitch threads from nominal diameter 8 mm to 39 mm within its scope.
What Is the Temperature Range for Nyloc Nuts?
ISO 2320 notes applications from −50 °C to +120 °C for conforming non-metallic-insert prevailing-torque steel nuts within its scope, but temperature affects functional behaviour. The specific product and service environment must still be validated.
Can Nyloc Nuts Be Reused?
Reuse should not be assumed. Repeated installation can change prevailing-torque behaviour, so the applicable product requirements, OEM maintenance policy and functional acceptance criteria should determine reuse.
Does Nyloc Nut Size Determine Tightening Torque?
No. Tightening torque also depends on the mating bolt, mechanical properties, coating, lubrication, friction, joint design and required preload. Do not select tightening torque from Nyloc Nut Size alone.
Is a Nyloc Nut Vibration Proof?
No. A Nyloc-type nut provides prevailing torque that can help resist unintended rotation, but joint performance still depends on preload, vibration, temperature, mating components and installation.
Questions Buyers Should Ask Before Ordering
Ask:
- What Nyloc Nut Size is required?
- Coarse or fine pitch?
- Regular, high or thin?
- Which product standard?
- Steel or stainless?
- What mechanical requirement?
- What insert requirement?
- Which coating?
- What mating bolt?
- What bolt coating?
- What temperature?
- Any chemical exposure?
- What prevailing torque is required?
- Is reuse allowed?
- What testing is required?
- Is PPAP required?
Before approving Nyloc Nut Sizes, confirm:
Thread + Pitch + Nut Type + Standard + Dimensions + Material + Mechanical Requirement + Insert + Coating + Bolt + Temperature + Prevailing Torque + Testing
Nyloc Nut Size Is Only the Starting Point
Choosing the correct Nyloc Nut Sizes begins with the mating bolt, but it should not end there.
The complete engineering sequence is:
Thread → Pitch → Nut Type → Standard → Dimensions → Mechanical Properties → Material → Insert → Coating → Bolt → Temperature → Prevailing Torque → Tightening → Testing
An M8 or M10 Nylon Insert Lock Nut can have the correct thread and still be unsuitable if:
- The wrong nut family is selected.
- Mechanical properties do not match the bolt.
- Temperature exceeds validated conditions.
- The insert is chemically incompatible.
- Coating changes assembly behaviour.
- Prevailing torque is outside the required range.
- Tightening does not produce the required joint condition.
- Reuse is uncontrolled.
For automotive, machinery, equipment and automation applications, buyers should qualify the complete nut-bolt-joint system, not only the thread size.
Rajal Industries can evaluate standard and customer drawing-based Nyloc Lock Nut and non-metallic-insert Locking Nuts for OEM applications, subject to technical feasibility, manufacturing process, tooling and sample validation.
Need Help Selecting Nyloc Nut Sizes?
Send Rajal Industries:
Drawing + Thread + Pitch + Product Standard + Nut Type + Material + Mechanical Requirement + Insert Requirement + Coating + Mating Bolt + Temperature + Prevailing-Torque Requirement + Testing + Quantity
for technical feasibility and quotation review.